
Uneven wall thickness in PET stretch blow molding usually reflects an imbalance in preform heating, stretching, air timing, alignment, or the starting preform itself. Diagnose the location and repeatability of the thin region before changing settings. Use a measured thickness map, cavity identification, and controlled trials to distinguish a process problem from a tooling or material problem.
Is Every Thickness Difference a Defect?
A bottle is not normally designed with identical thickness everywhere. The base, shoulder, sidewall, and reinforced features have different structural jobs. The relevant question is whether material distribution meets the approved design and performance requirements.
A visually attractive bottle can still have a weak local region, while a visible thickness transition may be intentional. Compare measured values with the packaging specification and reference samples. Include performance after filling, capping, handling, and storage rather than judging an empty bottle by appearance alone.
Establish how measurements will be taken before comparing production runs. Different contact pressure, probe placement, or sectioning methods can create apparent differences. Calibrate the instrument and use a repeatable map around the circumference and along the bottle height.
What Does the Defect Pattern Tell You?
Identify each sample by cavity, production time, preform lot, and recipe. Mark its orientation relative to the mold when that is practical. A pattern that repeats on one side of one cavity suggests a different investigation from a gradual change across every cavity.
| Observed Pattern | Checks to Prioritize |
| One side consistently thinner | Heating symmetry, preform rotation, alignment, and starting wall distribution |
| Shoulder or base repeatedly short of material | Axial heat profile, stretch motion, and pre-blow sequence |
| One cavity differs from the others | Local tooling, rod condition, valves, cooling, and transfer position |
| All cavities drift over time | Oven stabilization, incoming preform temperature, utilities, and ambient changes |
| Random bottles vary | Preform variation, intermittent feeding or rotation, and inconsistent process timing |
These patterns guide inspection; they do not prove a single cause. Several faults can produce a similar thin area. Preserve representative good and defective samples so the investigation has a stable comparison point.
How Does the Heating Profile Move Material?
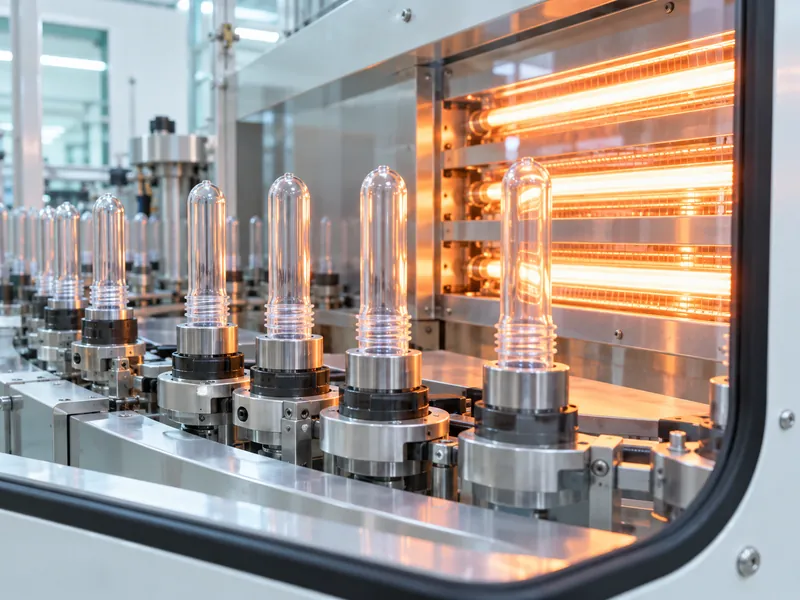
Heating determines how readily different regions of the preform stretch. A relatively hot area may deform earlier and become thinner, while a cooler area may retain more material. The actual result depends on the full stretching sequence and bottle geometry, so a simple increase or decrease in oven power can move the problem elsewhere.
Check individual lamp operation, reflector condition, ventilation, preform spacing, and rotation before rewriting the recipe. Dirty reflectors or a preform that stops rotating can produce an asymmetric temperature distribution. Compare the physical condition of the oven with the condition under which the approved recipe was established.
Review the incoming temperature of the preforms and the warm-up procedure. Material arriving from a cold storage area may not respond like material held near a warm production line. Establish a controlled preparation method rather than letting operators compensate for every delivery with undocumented oven changes.
Surface temperature measurements require care because transparent polymers and reflective surroundings can complicate interpretation. Use the equipment supplier’s approved measurement method and correlate readings with bottle results. Treat the temperature reading as evidence within the investigation rather than a complete description of the preform temperature through its wall.
Can the Preform Be Responsible?
Inspect preform weight, dimensions, concentricity, and wall distribution using the agreed incoming specification. A preform with uneven starting material can carry that imbalance into the finished bottle. Mixing lots or resin specifications can also change the response to an otherwise unchanged recipe.
Compare suspect material with an approved retained lot under controlled conditions. Record which variables remain fixed and keep enough samples to see whether the difference is repeatable. Do not approve a new preform merely because one trial bottle looks acceptable.
The preform must also suit the bottle’s geometry and filling application. A difficult material-distribution problem may originate in an unsuitable preform design rather than an operator’s settings. Review the combination with the preform and mold suppliers before assuming that extra heating can overcome every design mismatch.
How Do Stretching and Pre-Blow Affect the Result?
The stretch rod and initial air stage influence how the heated material begins to expand and where it first contacts the mold. Changes in rod motion, pre-blow timing, or pressure can alter axial and circumferential distribution. Because rod motion and air delivery act on the same heated preform, a trial that changes both without a defined experimental plan may leave the team unable to identify what improved the bottle.
Check rod straightness, centering, tip condition, travel, and the approved mechanical setup. A worn or misaligned component can create a recurring distribution problem that recipe changes only conceal. Follow the manufacturer’s isolation procedure before inspecting moving parts or pressurized components.
Review actual pressure behavior and valve timing where the machine provides suitable measurements. A recipe value does not guarantee that the intended pressure reaches the bottle at the intended moment. Restrictions, leaking seals, or inconsistent valve behavior deserve investigation when a previously stable process changes.
What Role Do the Mold and Cooling System Play?
Inspect mold alignment, seating, base components, vent condition, and cooling performance. A cavity that departs from the approved mechanical or thermal condition may produce a different contact pattern or surface result even when the shared machine recipe has not changed. Document cavity-specific findings so a repair can be linked to a subsequent production result.
Confirm that cooling circuits receive the specified flow and temperature under production load. A satisfactory chiller display does not establish that every mold passage is performing correctly. Blockage, a kinked hose, or an incorrectly connected circuit can affect one location while the main system appears normal.
Do not enlarge vents, polish cavity surfaces, or modify cooling passages without the tooling supplier’s approval. Small uncontrolled changes can affect dimensions, surface quality, or future repair options. Separate routine cleaning from operations that alter the tool.
What Is an Efficient Troubleshooting Sequence?
First contain the affected production and establish the last acceptable check. Confirm that the measurement method is reliable, then map the defect by position, cavity, and time. Review recent changes in material, maintenance, recipes, utilities, and production speed.
Restore obvious equipment faults before attempting process optimization. For a controlled trial, change one justified variable or one explicitly planned group of linked variables, then allow the process to stabilize. Record the settings and measure a sufficient sample from every relevant cavity.
Evaluate the result against the whole package requirement, not only the original thin spot. Improving one region may weaken another or change capacity and dimensions. Retain the previous approved recipe so an unsuccessful trial can be reversed without reconstructing it.
How Should the Corrected Process Be Released?
Confirm the thickness distribution and the application-specific strength tests over a representative production run. Include restarts and the operating conditions that previously triggered the defect. Set sampling frequency according to the risk and the stability demonstrated during qualification.
When discussing a PET blowing machine configuration, provide bottle drawings, preform details, and acceptance criteria rather than only requesting a nominal speed. The supplier needs these inputs to assess the process window. Agree how changes to tooling or material will trigger renewed qualification.
Finally, verify performance on the filling line, especially when reducing bottle weight. The handling considerations in running lightweight PET bottles through a filling machine remain relevant after a blowing adjustment. A stable, documented process must deliver both acceptable bottle measurements and reliable downstream behavior.