
PET bottle neck deformation can result from excessive heat exposure, inadequate neck protection, incorrect support or alignment, mechanical damage, or an out-of-specification incoming preform. First identify when the neck changes shape and whether the pattern follows a cavity, handling position, or material lot. Correct the demonstrated cause and verify sealing performance before releasing production.
Why Should the Neck Retain Its Original Geometry?
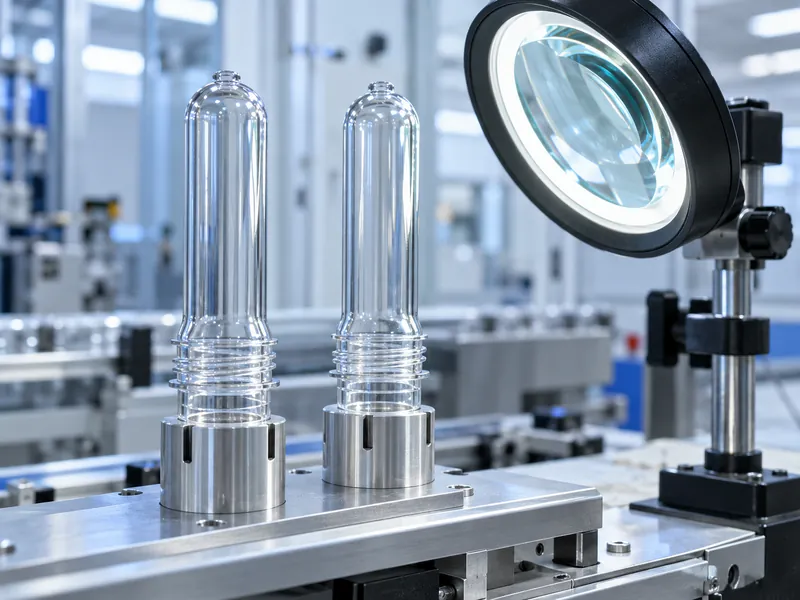
In normal two-stage stretch blow molding, the threaded finish is already formed in the injected preform. The reheating and blowing process shapes the body while preserving the functional neck dimensions. The finish must continue to fit its closure and the equipment that supports or transfers it.
Small changes can affect sealing, cap application, tamper evidence, or handling even when the bottle body looks acceptable. A bottle may also pass an informal cap-fit check while failing a defined dimensional or leakage test. Assess the neck against the approved package drawing and closure requirements.
Distinguish changes to the threaded finish from deformation of the shoulder immediately below it. A distorted shoulder calls for examination of body formation, whereas a damaged sealing finish calls for measurements tied to the neck and closure interface. Photograph the location and use consistent terminology so operators, quality staff, and suppliers investigate the same feature.
How Do You Identify the Stage Where Damage Appears?
Compare samples from incoming preforms, the relevant heated or transferred stage where safe sampling is supported, and finished bottles. Follow the machine manufacturer’s sampling procedure and never reach into moving equipment. The objective is to locate the earliest point at which the defect can be demonstrated.
Record the cavity, carrier or transfer position where available, production time, recipe, and preform lot. A defect that repeats at one handling position may require a mechanical investigation. A gradual change across the machine after warm-up may justify closer attention to heat accumulation and ventilation.
Keep good samples from the same run as well as defective ones. Compare them using the same conditioning time and measurement method. This reduces the risk of attributing a measurement difference to the process when it actually comes from inconsistent sample preparation.
What Neck Defects Should Be Measured?
| Observed Condition | Useful Checks |
| Oval Opening | Roundness, support contact, heat exposure, and handling forces |
| Damaged Threads | Incoming condition, gripper contact, transfer alignment, and closure fit |
| Distorted Sealing Surface | Finish dimensions, nozzle contact, temperature history, and leak performance |
| Bent or Damaged Support Ring | Carrier geometry, jams, impact marks, and preform specification |
| Shoulder Distortion Below the Neck | Heating profile, stretching, material distribution, and mold setup |
Use instruments and fixtures suitable for the feature being measured. A caliper reading alone may not fully characterize ovality or a sealing surface. Where the drawing does not define a sufficient inspection procedure, obtain a documented method from the packaging team and the supplier responsible for the cap-to-neck interface.
Document whether defects are cosmetic, functional, or both. Appearance remains relevant, but release decisions should include the features that affect package integrity. Retain the actual failed samples when discussing a recurring problem with the equipment supplier.
How Can Excess Heat Reach the Neck?
The oven must heat the preform body while shielding or cooling the finish sufficiently for the approved process. Incorrect lamp positioning, damaged protection components, unsuitable settings, or poor ventilation can expose the neck to excessive heat. A recipe that worked with another preform may not provide the same protection for a changed geometry.
Inspect shields, supports, airflow paths, and the cleanliness of the heating area. Compare their condition and position with the approved setup. Do not compensate for a damaged shield by repeatedly reducing overall heat until the bottle body can no longer form correctly.
Check how the defect evolves from startup to sustained running. Heat may accumulate around the neck-support arrangement or change after a production stop. Include restart behavior in the investigation when defects appear after interruptions rather than during steady output.
Verify incoming preform temperature and the consistency of storage-to-production handling. A change in starting condition can alter the heating response. Record those conditions before deciding that the oven controller itself is at fault.
Can Support Parts and Transfer Alignment Distort the Finish?
Incorrect or worn handling parts can load the neck or support ring in unintended ways. Confirm that carriers, grippers, guides, and nozzle interfaces match the approved finish. Verify the installed component against its approved part number and drawing, because visual resemblance does not establish that it supports the finish at the intended location.
Inspect for contact marks, burrs, loose components, and evidence of jams. Have trained personnel isolate the equipment and perform the prescribed alignment inspection before it returns to service. Avoid adjusting moving parts while trying to observe a defect at production speed.
Pay attention to changes made during maintenance or format conversion. Incorrect assembly, mixed change parts, or a connection restored in the wrong position can explain a sudden problem. Compare the installed parts with their identifiers rather than relying on the recollection of the last changeover.
If the problem follows one cavity, inspect its local nozzle, support, and related mechanical setup. If it follows a carrier through several stations, investigate that carrier and its path. The pattern can help narrow the work before unrelated settings are changed.
Could the Preform Arrive With the Defect?
Inspect retained incoming preforms from the affected lot before assuming that blowing created the condition. Shipping damage, improper storage, or variation in the supplied finish can affect the result. Confirm the part identity, drawing revision, and supplier release information.
Compare suspect and approved lots under the same documented setup if a controlled trial is appropriate. Keep the material separated and preserve traceability to the bottles produced. A successful trial with one lot does not automatically release another lot with different measured characteristics.
Provide the preform supplier with measurements and photographs rather than only a statement that caps do not fit. Include the frequency and location of defects in the sampled shipment. This helps distinguish a geometry issue from damage caused by transport or factory handling.
What Should You Avoid During Troubleshooting?
Do not assume that increasing blowing pressure will restore a neck that should not have been reshaped. Refer any proposed machining or alteration of neck-contact hardware to the equipment manufacturer before work begins, with the intended change described on a controlled drawing. Such changes can introduce new loads or remove the evidence needed to understand the original fault.
Avoid changing several unrelated settings at once. Start with the evidence from the defect pattern, inspect the relevant hardware, and define a controlled trial. Save an identifiable copy of the last qualified recipe before testing, including the values needed to restore production if the new setup fails its checks.
Do not send suspect bottles to filling merely because the cap can be forced onto them. Confirm the specified dimensions and functional package checks. Contain affected production according to the plant’s release procedure while the investigation is incomplete.
How Should the Corrective Action Be Verified?
Repeat dimensional and functional checks on bottles from every relevant cavity or handling position. Include sustained production, normal stops, and representative restarts. Inspect body dimensions and observe the approved transfer sequence after the neck issue has been corrected, so the release covers the complete bottle and its movement through the machine.
Test the intended closure under the approved capping conditions and evaluate leakage and opening behavior. Where lightweight bottles are used, also review the downstream handling conditions described in running lightweight PET bottles on a filling line. The corrected finish must perform through the actual line and package life.
Update the setup record, maintenance instruction, or incoming inspection requirement that addresses the confirmed cause. Train the people who will repeat that work. A repair is less dependable when its essential adjustment remains only in one technician’s memory.
What Information Helps a Supplier Resolve the Problem?
Send the machine model, neck and preform drawings, recipe, defect photographs, measurement results, and the pattern by cavity or time. Describe recent material and maintenance changes. For a PET bottle blowing system, this evidence is more useful than a request for a universal neck-temperature setting.
Agree the corrective trial and acceptance conditions before resuming normal release. Preserve the before-and-after records so future recurrence can be recognized quickly. The aim is a stable neck geometry and reliable seal under repeatable production conditions.