
Match an industrial labeling machine to the surface being labeled and the way the container can be controlled. Round bottles often suit rotational wrap applications, while oval and square bottles may need orientation and stabilization for panel labels. Tapered or flexible packages require a closer review because nominal bottle size alone does not describe application difficulty.
Package material alone cannot establish whether the proposed labeler suits the job. Ask whether it can place your chosen label on the intended part of your filled container at the required output. Two bottles made from the same material can need very different handling arrangements.
Why Is the Labeling Surface More Important Than Bottle Volume?
The label contacts a specific area of the body, not the container’s stated capacity. A nominal 500 ml bottle might have a straight label panel, a curved shoulder, molded ribs, or a tapered wall. Record the usable area directly instead of relying on the volume printed on a drawing.
Measure height and width of the proposed panel, body dimensions through that area, and distances to shoulders or recesses. Also note seams, embossing, grip features, and surface texture. These details help determine whether the artwork and label geometry leave enough practical clearance.
Take samples from normal production rather than sending only hand-selected perfect bottles. If molding variation affects the body, a trial should expose that variation within the agreed material specification. Otherwise, a successful sample run may not represent the delivered packaging.
When Does a Round Bottle Suit Wrap-Around Labeling?
A straight, stable cylindrical labeling area is a useful starting point for a wrap application. The process must control the bottle while the label follows its circumference. Contact, rotation, and timing need to remain consistent across the agreed bottle variation.
Decide whether the label should finish with a gap or an overlap. For a circular cross-section, circumference can be estimated as pi multiplied by diameter, but final label length must reflect the actual design and converter tolerances. Do not use that calculation alone to approve production artwork.
As an example, a 70 mm diameter gives a geometric circumference of approximately 219.9 mm. A proposed 210 mm label would leave about 9.9 mm before accounting for practical tolerances and actual bottle geometry. This is a design illustration, not a recommended seam allowance.
The BRENU labeling machine page presents wrap-around and double-sided placement options. Use your package samples to establish which arrangement is appropriate. Confirm any relationship the label must maintain to a seam, handle, or printed feature.
What Changes With Oval or Rectangular Bottles?
These containers often require controlled orientation before labels are applied. A panel label needs to meet the intended face consistently, and the package must remain stable while contact pressure is applied. Front and back positions should be assessed together.
Ask whether the machine receives randomly oriented containers or already aligned ones. That distinction can change the scope of the infeed considerably. A label head may be capable of the application while the proposed feeding arrangement remains unsuitable.
Filled weight and center of gravity also matter. A tall, narrow package may rock during transfer, while a flexible container may change shape under holding pressure. Test representative filled containers or a validated equivalent.
Why Do Tapered Containers Need Extra Attention?
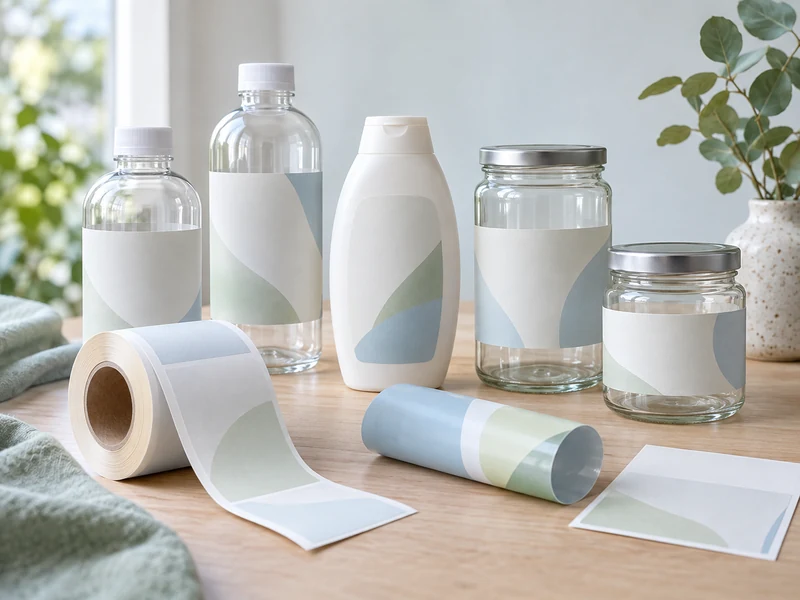
A tapered wall has a different circumference at different heights. A rectangular label spanning that wall may encounter unequal travel around its upper and lower edges. The result can require a modified label shape, a different application area, or another decoration method.
Measure the taper across the intended label height and review it with the label converter. A curved die-cut label may be appropriate for some applications, but its shape must be developed for the actual geometry. Avoid treating every wrinkle as a machine-setting problem.
If the artwork requires broader coverage over a shaped body, review the shrink sleeve option. A sleeve still needs validation of its final appearance and heat-processing conditions. It is an alternative to evaluate, not a universal correction for difficult geometry.
How Should You Assess Flexible PET or HDPE Packages?
Assess the container under the conditions it will experience during labeling. Empty and filled packages may respond differently to contact, and the product or closure can affect the overall stiffness. Tell the supplier whether trial containers represent the filled, capped, temperature-conditioned units that will actually reach the labeling station.
Record whether the package is warm, chilled, pressurized, recently filled, or subject to surface moisture. These conditions may affect handling or adhesion and should be reproduced where practical. If a test uses room-temperature samples, document the limitation.
BRENU’s carbonated filling-line overview provides context for chilled beverage workflows. Use it to locate the point where container condition is established before labeling. Assign responsibility for any conditioning needed between the filler and labeler.
What Should You Check on Glass Bottles and Jars?
Check actual dimensional variation, body features, and the relationship between the intended label area and the closure. A jar’s wide body does not guarantee a generous straight-wall panel. Some designs transition quickly into a shoulder or base radius.
For glass, evaluate the package’s normal manufacturing features rather than assuming a visually round body is perfectly cylindrical. Sample inspection should include the area where the label starts and finishes. Define acceptable appearance with retained examples.
For jars with a lid or tamper feature near the label, confirm that the label does not interfere with opening or inspection. Keep decorative placement requirements separate from any closure-integrity requirement. The machine proposal should state exactly which application it supplies.
Which Package Variations Belong in the Trial?
Choose samples that challenge different aspects of the application. The smallest bottle, longest label, lightest package, and most pronounced taper may be four different SKUs. Testing only the largest and smallest volumes can miss the actual difficult combinations.
| Package Feature | Trial Question | Evidence to Record |
| Straight round body | Does the wrap finish consistently? | Leading edge, trailing edge, and seam measurements |
| Oval or rectangular body | Does the correct face stay presented? | Front/back alignment and orientation stability |
| Tapered label area | Does the label lie as designed? | Edge lifting, wrinkles, and approved label geometry |
| Flexible or lightweight bottle | Does handling alter its shape or balance? | Transfer behavior and application consistency |
Define appearance after the relevant downstream handling as well. A label that passes at discharge may later scuff or lift during grouping. Coordinate those checks with the chosen shrink-wrapping or carton-packing process.
Where Should Barcodes Be Evaluated?
Evaluate them on the finished package and in the relevant scanning conditions. Position, shape, and decoration can influence how the symbol is presented. Do not approve the application only from a flat artwork proof.
GS1’s 2D retail implementation guideline explains that the full 2D symbol must be captured and discusses the effects of curvature and surface conditions. Coordinate the code area with the artwork and packaging specialists. Avoid placing the critical code where the chosen application process creates unnecessary distortion or obstruction.
Use an agreed verification method and retain the result with the package sample. A single successful scan is useful for a quick check, but it is a narrow observation. Acceptance should reflect the requirements of the intended supply chain.
How Should You Manage Container Variation Within One Format?
Qualify the permitted variation within a container specification as well as the nominal design. Samples from one small batch may not show all the dimensional or surface differences that arrive during regular purchasing. Ask the container supplier which characteristics are controlled and how representative samples should be selected.
For example, a rectangular bottle may share its overall dimensions with another lot while the useful panel or molded seam differs slightly. That difference can matter if label edges sit close to the panel boundary. Review the labeling area itself instead of approving compatibility from overall height and width alone.
Keep the agreed incoming limits realistic and measurable. If the equipment trial reveals a sensitivity to one feature, record it in the packaging specification and confirm who checks it. This prevents a successful sample test from becoming an unsupported promise to process every visually similar bottle.
What Happens When Several Shapes Share One Line?
Build a matrix that distinguishes common settings from required change parts. Grouping formats by similar handling needs can simplify production planning. It may be more useful to define a few validated format families than to promise unlimited flexibility.
Review this matrix against the complete water bottling workflow when changes affect upstream or downstream equipment too. A fast labeler changeover does not establish the total line changeover time. Agree on the last acceptable package of one format and first acceptable package of the next as the production boundary.
Send BRENU drawings, production samples, label files, and the intended operating conditions for each family. Ask which adjustments are routine and which changes require tooling or further trials. A useful recommendation should connect every claimed format capability to a defined package and an observable application result.